Top Rotary Screw Compressor Oil for Global Buyers?
Choosing the top rotary screw compressor oil is not a simple brand comparison. Global buyers must examine compressor design, operating temperature, duty cycle, and manufacturer requirements. A lubricant that performs well in a cool workshop may fail sooner in a dusty factory or tropical plant. The details matter.
Ron Marshall, a respected compressed-air systems specialist, offers a practical reminder: “Compressor oil is the lifeblood of the machine.” His point reflects real maintenance experience. Rotary screw compressor oil lubricates bearings, seals internal clearances, removes heat, and carries contaminants toward the filtration system. If its viscosity is unsuitable, discharge temperatures can rise. If oxidation resistance is weak, varnish may appear on valves, separators, and internal surfaces.
The best choice is not always the most expensive product. It should match the OEM specification, expected oil-change interval, and local service conditions. Buyers should compare mineral, PAO, ester, and other synthetic formulations carefully. Check safety data, technical data sheets, compatibility, and genuine supply channels. A low price can hide higher consumption.
There is no universal winner.
Even experienced buyers can overlook water exposure, frequent cycling, or long idle periods. These conditions change oil performance. A realistic evaluation should consider total cost, not only the price per drum. Reliable evidence includes field history, laboratory testing, and documented compatibility with the compressor model. This guide examines those factors for international purchasers seeking dependable rotary screw compressor oil, while acknowledging one uncomfortable truth: product claims still require verification in the actual machine.
What Is Rotary Screw Compressor Oil and Why Does It Matter?
Top Rotary Screw Compressor Oil for Global Buyers?
What Is Rotary Screw Compressor Oil and Why Does It Matter?
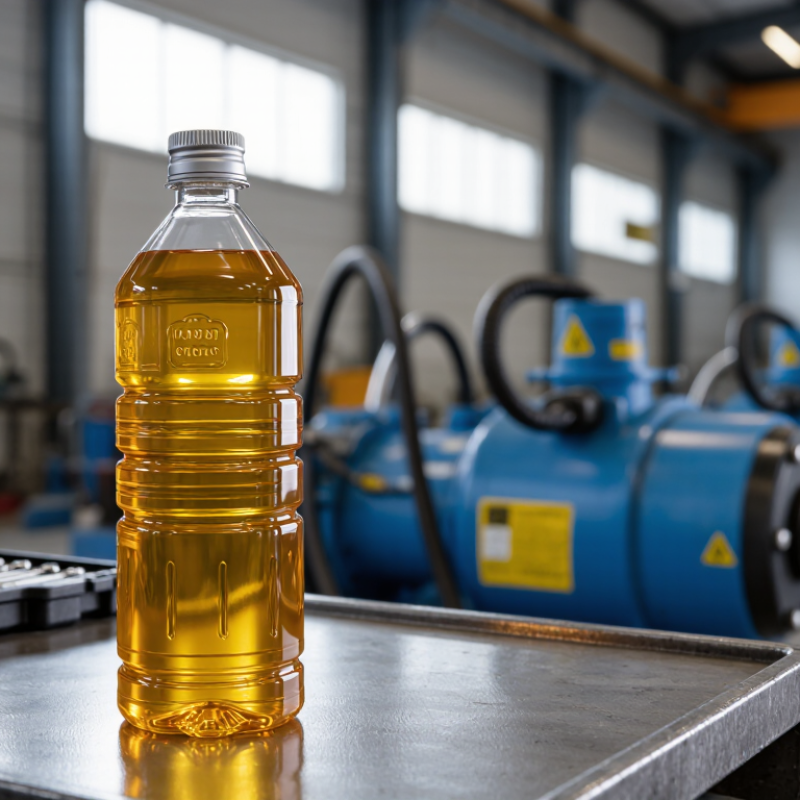
Rotary screw compressor oil is a working fluid, not merely a lubricant. It reduces friction between rotating air ends. It also seals internal clearances, removes heat, and protects bearings from wear. In many oil-injected compressors, oil quality directly affects discharge temperature and energy stability. A wrong product can create varnish, foaming, or excessive oil carryover.
Selection should match the compressor manual, operating temperature, speed, and service interval. Viscosity matters. So does oxidation resistance. Mineral oil may suit lighter duty, while synthetic oil can support longer, hotter operation. However, synthetic does not automatically mean better. Compatibility with seals and existing oil is essential. Mixing fluids without technical confirmation can cause deposits or separation.
Watch the machine, not only the container. Check oil level, pressure, temperature, and unusual drain color. A clean-looking sample may still be chemically tired. Laboratory analysis can reveal moisture, metal particles, and viscosity changes before failure occurs. Dusty sites may need shorter intervals. Humid rooms deserve closer water monitoring. Field technicians sometimes trust long replacement schedules too much; real conditions often disagree. No oil choice is perfect. It should be verified through records, sampling, and steady performance.
A practical comparison of common lubricant types, viscosity grades, operating characteristics, and selection factors for oil-injected rotary screw compressors.
| Oil Category | Base Fluid | Common ISO VG Grades | Typical Strengths | Typical Limitations | Indicative Service Interval* | Best-Fit Operating Conditions | Buyer Verification Checklist |
|---|---|---|---|---|---|---|---|
| Mineral Compressor Oil | Highly refined mineral oil with an antioxidant, anti-rust, anti-foam, and anti-wear additive system. | ISO VG 32 ISO VG 46 ISO VG 68 | Cost-effective initial purchase; widely available; suitable for many standard-duty air compressors when approved by the equipment manufacturer. | Generally shorter oxidation life than synthetic fluids; more sensitive to high discharge temperatures, contamination, and extended drain periods. | Commonly about 2,000–4,000 operating hours, depending on temperature, contamination, oil quality, and compressor instructions. | Normal ambient conditions, moderate duty cycles, and applications where regular oil changes are practical. | Confirm the manufacturer’s approval, viscosity at operating temperature, oxidation stability, and compatibility with seals and residual oil. |
| PAO-Based Synthetic Oil | Polyalphaolefin synthetic base fluid, normally combined with a performance additive package. | ISO VG 32 ISO VG 46 ISO VG 68 | Good oxidation resistance, strong low-temperature flow, reduced volatility, and broad operating-temperature capability. | Higher purchase price; some formulations may have limited compatibility with certain elastomers or residual lubricant types. | Commonly about 4,000–8,000 operating hours when the compressor maker permits extended service and conditions are controlled. | Variable ambient temperatures, frequent starts, continuous operation, and applications requiring longer lubricant life. | Check compatibility with seals, hoses, filters, separators, and any remaining mineral oil before conversion. |
| Ester-Based Synthetic Oil | Synthetic ester base fluid formulated for compressor lubrication and thermal-oxidative stability. | ISO VG 32 ISO VG 46 ISO VG 68 | High lubricity, good solvency for some deposits, and strong performance in demanding temperature conditions when properly formulated. | Formulation-dependent material compatibility; some ester chemistries can be sensitive to moisture or hydrolysis; usually higher cost. | Commonly about 4,000–8,000 operating hours, but the actual interval must be established by oil analysis and manufacturer guidance. | High-load or high-temperature service where an approved ester formulation is specified. | Verify ester type, water tolerance, seal compatibility, additive chemistry, and the compressor manufacturer’s written approval. |
| PAO/Ester Blend | Combination of PAO and ester synthetic base fluids designed to balance oxidation stability, lubricity, and additive solubility. | ISO VG 32 ISO VG 46 ISO VG 68 | Often provides a balanced combination of thermal stability, low-temperature performance, lubricity, and additive compatibility. | Performance varies significantly by formulation; not every blend is suitable for every compressor or seal material. | Commonly about 4,000–8,000 operating hours under suitable conditions and with approved equipment. | Industrial plants with continuous duty, fluctuating temperatures, or a preference for synthetic service intervals. | Request the technical data sheet, safety data sheet, compatibility statement, and recommended drain procedure. |
| Food-Grade Compressor Lubricant | Mineral or synthetic base fluid formulated and registered for incidental food-contact environments, commonly using an appropriate H1 classification where applicable. | ISO VG 32 ISO VG 46 ISO VG 68 | Supports hygiene requirements in food, beverage, pharmaceutical, and packaging environments when the complete lubrication program is properly controlled. | Food-grade status does not mean the lubricant is harmless for consumption; performance, service life, and compatibility depend on the specific formulation. | Determined by the lubricant approval, compressor manufacturer, oil analysis, and site hygiene program; do not assume a longer interval. | Areas where incidental contact with compressed air or equipment surfaces is a compliance concern. | Confirm the applicable registration or certification, incidental-contact category, viscosity, allergen policy, and audit documentation. |
| Biodegradable Compressor Lubricant | Typically based on synthetic esters or other readily biodegradable fluids, with additives selected for compressor service. | ISO VG 32 ISO VG 46 ISO VG 68 | Can reduce environmental persistence in applications where accidental release or ecological exposure is a concern. | Moisture sensitivity, hydrolytic stability, storage life, and seal compatibility can vary; not all biodegradable oils are interchangeable. | Often established by oil analysis and the supplier’s recommendation rather than by a universal fixed-hour interval. | Environmentally sensitive sites, outdoor equipment, marine operations, and locations with strict spill-management requirements. | Verify biodegradability test method, environmental classification, water tolerance, storage requirements, and equipment approval. |
| ISO VG 32 | Low-viscosity compressor oil grade. | 32 cSt at 40°C | Easier cold starting and lower fluid resistance in suitable low-temperature or manufacturer-approved applications. | May provide insufficient film thickness at high operating temperatures or under heavy load if the compressor requires a higher grade. | Not applicable as a lubricant type; service life depends on the base fluid and formulation. | Cooler climates, low-temperature starts, or equipment specifically designed for this viscosity. | Check the compressor manual, minimum start temperature, discharge temperature, and operating-load requirements. |
| ISO VG 46 | Medium-viscosity compressor oil grade. | 46 cSt at 40°C | Common general-purpose viscosity for many oil-injected rotary screw compressors operating in moderate conditions. | May be too thick for some cold-start conditions or too thin for certain high-temperature, high-load designs. | Not applicable as a lubricant type; service life depends on the base fluid and formulation. | Moderate ambient temperatures and standard industrial compressed-air service when specified by the manufacturer. | Confirm that ISO VG 46 is specified rather than selecting it solely because it is widely used. |
| ISO VG 68 | Higher-viscosity compressor oil grade. | 68 cSt at 40°C | Can provide a thicker lubricating film in approved high-temperature or higher-load applications. | Increased resistance during cold starting and potentially higher power consumption if used where a lower grade is required. | Not applicable as a lubricant type; service life depends on the base fluid and formulation. | Warmer environments or compressor designs that specifically call for a higher viscosity. | Verify pumpability, start-up temperature, motor load, and the equipment maker’s required viscosity range. |
Related Posts
-
2026 Best Compressor Oil for Global Buyers Insights?
-

What Is the Best Rotary Screw Compressor Oil in 2026?
-
How to Choose the Right Screw Compressor Oil for Your Needs?
-
Essential Tips for Choosing Rotary Screw Compressor Oil?
-
Why is Choosing the Right Compressor Oil Important for Efficiency?
-
2026 How to Choose the Best Screw Compressor Oil for Longevity?